News

Latest updates from Quanzhou Northern Garment, including OEM & ODM apparel manufacturing, factory developments, product updates, quality and compliance, and industry insights for global B2B buyers.

White cotton bales stacked in a textile mill warehouse with greige fabric rolls, illustrating 2026/27 cotton supply constraints from climate and rising input costs

Cotton Supply Squeeze 2026/27 Reshapes Fabric Sourcing for OEM/ODM

08/18/2026

Global cotton supply is heading into another contraction. According to Ecotextile News' latest field reporting, total cotton area worldwide is forecast to decline in the 2026/27 marketing year as farmers respond to three compounding pressures: rising input costs (fertiliser, fuel, irrigation), persistent drought in major growing regions, and tougher competition from man-made fibres on price-performance grounds.For brands and buying teams planning SS27 and AW28 cotton-heavy collections, the practical effect is that traditional cotton sourcing calendars will no longer hold. Fibre availability, not just price, is becoming the binding constraint. Mills that locked forward contracts in Q1 2026 are now reporting reduced allocation, and spot cotton quotes are showing wider regional spreads than at any point in the past three seasons.For a Quanzhou-based OEM/ODM partner, the response is a layered one. Drawing on more than a decade of mill relationships in Jiangsu, Shandong and Anhui, our sourcing team is taking three concrete steps with buyers for the upcoming seasons:Forward booking earlier in the season. Where buyers confirm 60% of the volume at tech-pack sign-off rather than at PO, we can lock yarn allocation with the mill. The cost premium is typically 2-4% but the supply security is real, especially for ringspun and combed cotton counts that run on tighter capacity.Blending as a design strategy, not a fallback. Cotton-polyester, cotton-modal and cotton-recycled blends are being engineered at the yarn stage to keep the hand-feel and dye uptake of cotton while reducing exposure to spot market volatility. Buyers who treat blending as a deliberate design choice — for performance, drape, or sustainability — tend to be more satisfied with the result than those who treat it as a cost-down lever.Recycled cotton and GOTS-certified organic as risk hedges. The recycled cotton market has matured enough in 2026 that it can absorb meaningful volume for hoodies, sweatshirts and outerwear shells. For buyers with their own sustainability targets, this also creates a cleaner story for downstream DPP and CSRD reporting under EU rules coming online in 2027.The broader lesson is that cotton supply in 2026 is no longer a commodity call — it is a sourcing strategy. Buyers who treat their fabric sourcing as a fixed line item in the cost sheet will find themselves respecifying mid-season; buyers who treat it as a planning conversation with the factory from sampling onward will keep their collections on time.Northern Garment supports buyers at both ends: mill-direct fabric sourcing with documented chain-of-custody, and an in-house sampling team that can build and ship counter-samples within seven working days, including alternate-fabric substitutions. If your SS27 line is cotton-heavy and you want a second opinion on fibre allocation, our sourcing desk is open.Source: Ecotextile News, 2026-06-02

Global shipping container port at dusk with cargo cranes and freight ship, representing 2026 US Section 301 apparel tariff impact on Asian sourcing

US Section 301 Tariffs Reshape Asian Apparel Sourcing for OEM/ODM Buyers

08/18/2026

The United States Trade Representative has finalised a new wave of Section 301 tariffs covering 60 apparel-producing economies, and the reaction across Asia this week is less about the headline rates and more about the second layer of measures quietly tucked inside them. According to Sourcing Journal's analysis of the USTR announcement, 42 countries now sit in a 12.5% tariff band — including China, Vietnam, Japan, Thailand, South Korea, the Philippines and Singapore — while 18 countries, among them Sri Lanka, Bangladesh, Malaysia, India, Indonesia, Pakistan and Cambodia, are placed in a lower 10% band.For OEM/ODM buyers running multi-country sourcing, the most consequential change is not the percentage but the new textile mechanism. Garments assembled with U.S.-origin inputs, including U.S. cotton, can now enter the United States free of Section 301 duties. The provision is expected to benefit Bangladesh, Cambodia, Indonesia and Malaysia most directly, and is initially set to run for three years. Industry voices in India have already warned that tariff parity will mean little if competitors receive exemptions that India does not.For Quanzhou-based manufacturers, the message is straightforward: headline tariff rates are no longer the only variable. Three practical implications for OEM/ODM partners sourcing out of China in late 2026:Material origin is now a margin lever. Garments using U.S. cotton or other U.S.-origin textile inputs can be re-engineered to qualify for the new textile mechanism. Buyers asking for origin documentation will become the norm, not the exception.Dual-country routing will accelerate. Expect more buyers to test Vietnam or Bangladesh for next-season capacity while keeping China for technical outerwear and complex sampling. The factory that can speak to both setups wins the long-term relationship.Compliance documentation is now a sales tool. Traceability records, country-of-origin declarations, and forced-labour audit trails have moved from "nice to have" to table stakes for new RFQs.Vietnam's foreign ministry has already stated it will continue negotiations with Washington, and Bangladesh's commerce minister framed the new structure as a replacement of existing duties rather than an additional burden. Either way, U.S. demand is expected to soften as costs pass through, which makes supplier flexibility and short lead-time sampling more valuable than ever.For buyers building SS27 and AW27 lines, the right question is no longer "where is the cheapest country" but "which supplier can document origin, pivot between countries, and hold quality across both?" Northern Garment supports buyers through this transition with multi-origin material sourcing, full traceability documentation, and a sampling team in Quanzhou that can ship counter-samples within seven working days.Source: Sourcing Journal, 2026-08-15

Close-up of a custom-made light blue shirt collar showing precise stitching and embroidered monogram detail on a wooden hanger

Custom Apparel Details: 12 Things Buyers Should Look At Before Approving a Bulk Order

08/17/2026

The difference between a custom apparel order that ships on time and one that ends up in a claims folder usually traces back to a handful of details a buyer either specified clearly — or didn’t. At Quanzhou Northern Garment Co., Ltd., we work with private-label brands and buying offices on OEM (build to buyer’s tech-pack) and ODM (build to a brief) production for swimwear, outerwear, activewear and hoodies. After twelve years and tens of millions of garments, the same twelve details keep showing up on every well-run order, and their absence keeps showing up on every problematic one. This is the checklist we walk every new buyer through before a tech-pack is finalized. The details that define custom apparel: precise topstitching along the collar band, clean buttonhole, embroidered monogram, structured collar roll — every one of these is a checklist line item on a well-run custom order. 1. Fabric Specification: More Than a Composition Line “80% nylon / 20% spandex” is not a fabric spec — it’s a starting point. A buyer-ready fabric spec includes fiber composition, weight (GSM or oz/yd²), width (cuttable), stretch percentage and recovery, finished hand-feel (soft, firm, brushed, slick), color fastness ratings to the relevant agents (chlorine, sea water, light, perspiration), pilling grade, and any required certifications (OEKO-TEX Standard 100, GOTS, REACH compliance, recycled-content documentation). The clearer the spec, the fewer surprises when the lab-dip arrives. 2. Tech-Pack Completeness A tech-pack should function as a contract. The four sections that most often go wrong are: measurement spec (with tolerance, e.g. ±1 cm), construction notes (seam type, SPI, topstitch position), BOM (bill of materials — every trim, label, hardware item), and artwork files (vector for prints, separated by color). If any of these are vague, expect at least one round of revisions and added lead time. We have a one-page tech-pack template we share with buyers who are sourcing their first capsule. 3. Sample Rounds: PPS, Fit Sample, and Pre-Production Sample Buyers sometimes compress the sample stage to save time and end up costing a week downstream. The standard cadence for our lines is: a pre-production sample (PPS) made from bulk fabric and trims, couriered for buyer approval; a fit sample pulled from the first cut bundle to confirm the line is sewing to spec; and a final bulk-shipment reference sample retained in our archive for any future re-order. Each round has a defined approval window (typically 3 working days) — holding any of them up pushes the bulk date back by the same amount. 4. Stitch Quality and Seam Construction Stitch quality is the easiest thing to check and the most common reason a finished garment gets rejected. Look at the stitches per inch (SPI) — 10–12 SPI is typical for main seams, 8–10 for topstitch on woven outerwear, 14+ for elastic application on swimwear. Confirm seam type (4-thread overlock for stretch, 5-thread safety stitch for high-stress seams, lockstitch for crisp topstitch). Inspect buttonholes, bartacks at pocket corners, and the symmetry of collar points. These are the QC checks our line-walkers run on every bundle. 5. Trims and Hardware Buttons, zippers, snaps, hooks, sliders, drawstring tips, toggles, metal rings — every hardware item on the BOM should be sourced from an approved supplier with a documented specification (size, finish, tensile strength, color match against a Pantone or physical sample). Custom hardware usually adds 7–10 days to lead time and a tooling charge, so specify up-front. For swimwear, the choice between stainless steel and Zamac alloy rings matters for salt-water durability — a detail often missed in tech-packs. 6. Color Management Always reference a Pantone TPX / TCX number (or a physical swatch from the buyer) when specifying color. We dye or print to a lab-dip against that reference, send a swatch for approval, and only proceed to bulk once the buyer signs off. The acceptable ΔE (delta-E) tolerance should be agreed in writing — typically ≤ 1.0 for solid colors and ≤ 2.0 for printed grounds. Without that number, color approval becomes subjective and disputes become hard to settle. 7. Size Run and Grading Confirm the size run (e.g. XS–XXL, or 6 sizes for EU wholesale) and the grading rules — the increments between sizes, especially at the hip, waist, sleeve length and inseam. A common pitfall is grading proportionally off an arbitrary size block; the better approach is to anchor on a fit-approved sample (a “fit block”) and grade away from it. For private-label capsules targeting a specific demographic (e.g. women’s swimwear, ages 25–40), we recommend using a fit-tested block from a previous successful order rather than re-deriving one each season. 8. Print and Embroidery Artwork For sublimation prints, the artwork file should be vector or 300 DPI raster, supplied in CMYK with named spot colors and a clearly marked repeat size. For embroidery, the file should include stitch type (satin / fill / running), stitch direction, thread color references, and the finished embroidery size on the garment (often 5–8 cm for a chest logo). We send a sew-out / print-proof on bulk fabric for approval before production begins — this is the cheapest place to catch a registration or color-shift problem. 9. Packaging Details Packaging is part of the product, especially for retail-ready shipments. Specify: polybag type (clear OPP, individual vs. multi-pack), folding method (some buyers require a specific fold for shelf-ready presentation), hangtag position, size-strip on the polybag, and the master carton configuration (pieces per inner, inners per carton, carton dimensions, gross weight). Custom-printed polybags and hangtags typically carry a tooling fee and a 2-week lead time — order ahead of bulk. 10. Compliance and Labeling Every market has its own labeling rules. For the EU, fiber composition and country-of-origin must appear on the garment; for the US, the FTC Care Labeling Rule dictates care symbol content and placement; for swimwear sold into California, Prop 65 warnings may be required on certain hardware finishes. Confirm with your factory which care symbols standard they work to (ISO 3758 / ASTM / Ginetex) and which side of the garment they’ll be sewn on. 11. Shipping Terms and Lead Time Be explicit about the Incoterm — FOB Xiamen is our standard for export, EXW factory for buyers with their own logistics, CIF / DDP available on request. Lead time from deposit to ex-factory is typically 35–45 days for orders in the 2,000–10,000 piece range, but add 7–10 days for custom hardware or printed polybags. For urgent orders, sample-line capacity can be reserved up to four weeks in advance. 12. Communication Cadence The single biggest predictor of a smooth custom order is the communication cadence: who approves what, by when, and through which channel. We send weekly progress photos during production, an inline QC report at the 30% and 70% marks, and a final photo-loading report once the container is sealed. Buyers who respond within 24 hours on sample approvals and lab-dip sign-offs routinely take 5–7 days off their total lead time. Closing Note If you are evaluating a custom apparel partner for the first time, walking through these twelve points before signing a PO will save you the most common round of disputes on tech-pack gaps, color drift, packaging mismatches and lead-time slips. Send your tech-pack or a brief to our sourcing team for a same-week response, sample plan, and indicative pricing. Quanzhou Northern Garment Co., Ltd. — OEM/ODM custom apparel manufacturer based in Jinjiang, Fujian, China. Custom hardware, custom packaging, full private-label service. OEKO-TEX Standard 100 (year 8). Serving buyers in 20+ countries since 2013.

Garment workers sewing colorful swimwear on industrial sewing machines inside a clean Chinese apparel factory workshop

Inside Our Swimwear Manufacturing Process: From Fabric to Container Loading

08/17/2026

Behind every women’s swimwear order that lands on a retailer’s shelves sits a chain of decisions: which fabric to source, how to grade a pattern across six sizes, when to inline-inspect a seam, and how to load a 40HQ so it arrives at its destination without claim. At Quanzhou Northern Garment Co., Ltd. — a Jinjiang-based apparel manufacturer serving B2B buyers across Europe, North America, Australia and the Middle East for more than 12 years — that chain is broken into eight controlled stages. This article walks through each one, so sourcing teams and private-label brands can see exactly what happens between an approved tech-pack and a container sailing out of Xiamen. Step 1 — Fabric Sourcing & Lab Testing Every swimwear build begins with the fabric. We work with a curated list of Chinese mills (and selected Italian/Indonesian suppliers on request) that ship the four families our buyers ask for most: 80% Nylon / 20% Spandex — the mainstream choice for one-piece swimsuits and bikini briefs, soft hand-feel, matte finish.82% Polyester / 18% Spandex — preferred for sublimation prints, chlorine-resistant variants available.Recycled Nylon (REPREVE® / ECONYL®) — for buyers building a sustainability story into the collection.Lining fabrics — power mesh for tummy-control panels, lightweight nylon lining for cupping. Every fabric lot is logged with a batch code and sent to our in-house lab for the four tests that matter most for swimwear: color fastness to chlorinated water, color fastness to sea water, UV protection (UPF 50+ where required), and AZO-free / REACH compliance. OEKO-TEX Standard 100 certification — currently in its eighth year of annual renewal — covers the full fabric library our production lines draw from, and reports can be attached to every shipment on request. Step 2 — Pattern Making & Sample Development Once the buyer’s tech-pack lands, our pattern makers translate it into graded CAD files across the buyer’s size run (typically XS–XXL, or 6 sizes for European wholesale). Two physical fit samples are produced before bulk: a pre-production sample (PPS) shipped by express courier for buyer approval, and an inline fit sample pulled from the first cut batch for in-line verification. Standard lead time from tech-pack receipt to PPS dispatch is 7–10 working days, including one round of pattern revision at no charge. Buyers working on their first private-label swimwear capsule typically start at 300–500 pieces per style per color to validate the fit before scaling. Step 3 — Spreading & Cutting Cut planning starts with a marker that minimizes fabric waste, typically 87–92% material utilization depending on style complexity. Fabric is spread on long cutting tables in layers of 30–80 plies (depending on fabric weight and stretch), then cut using computer-controlled straight knives and band knives for curved panels. Each cut bundle is bar-coded with the style, color, size and lay number so it can be traced back to the exact fabric lot through every downstream station. Step 4 — Printing, Sublimation & Solid Dye For printed swimwear (the majority of our orders), heat-transfer sublimation printing is the default. Artwork files from the buyer are color-separated in-house, printed on transfer paper, and pressed onto polyester-blend fabric at 200 °C. For solid colors, we work with reactive-dye mills for color accuracy across production lots. All printed panels are inspected under D65 light booths against the buyer-approved lab-dip before they move to sewing. Step 5 — Sewing: The Heart of the Garment Sewing is where most swimwear quality issues are won or lost. Our swimwear lines run four-thread overlock machines for main seams (which deliver stretch plus durability), coverstitch machines for hems, and dedicated elastic-application stations for waistbands, leg openings and under-bust bands. Hardware — metal rings, sliders, hook-and-eye closures, plastic adjusters — is sourced from approved suppliers and applied in a separate sub-line to keep the main assembly flow clean. An average bikini set involves 18–22 sewing operations; a one-piece with tummy-control lining can run to 35. Line balancing — assigning the right number of operators to each operation so the bundle flows without bottlenecks — is what keeps our standard swimwear line at a daily output of 1,800–2,400 finished pieces per line without compromising on the four-point inline checks performed at every station. Step 6 — Inline & Final Quality Control QC happens in two layers. Inline QC is performed by station-checkers walking the line: seam type and SPI (stitches per inch), elastic stretch recovery, print registration, hardware attachment. Final QC takes place on a dedicated inspection table under D65 lighting, with each piece checked against an AQL 2.5 sampling plan (General Inspection Level II) for defects such as skipped stitches, broken needles (recorded via the needle-control log every shift), fabric flaws, and measurement drift outside the spec sheet tolerance of ±1 cm. Buyers ordering for the EU market can request metal-needle detection on the final line at no additional charge — a small step that has saved more than one shipment from a costly recall. Step 7 — Folding, Polybag & Carton Packing Approved pieces are folded to a standard presentation, individually sealed in OPP polybags (custom-printed polybags and hangtags available on request for orders above 1,000 pieces per style), and packed into export cartons sized for either a 20ft or 40ft HQ container. Standard inner-pack is 6 pieces per polybag inner, 4 inners per carton = 24 pieces per master carton, but we adjust to the buyer’s retail-floor planogram where required. Step 8 — Container Loading & Shipment Cartons are palletized, stretch-wrapped, and loaded into containers by our logistics team at the Jinjiang factory gate, with photographic loading reports sent to the buyer at completion. A typical 40HQ holds roughly 28,000–32,000 bikini sets depending on packaging density, and a typical 20ft holds about half that. We ship FOB Xiamen as standard, with EXW factory and CIF/DDP quotes available on request. Lead time from deposit to ex-factory is typically 35–45 days for orders in the 2,000–10,000 piece range. What This Means for Buyers Sourcing From Us If you are a private-label brand, a buying office, or a wholesaler evaluating swimwear suppliers, the workflow above is what you can expect on every order — from the first sample courier to the last carton loaded at our gate. We support OEM (build to buyer’s tech-pack) and ODM (develop from your brief into tech-pack and samples) for women’s, men’s and children’s swimwear, with an MOQ starting at 300 pieces per style per color for development runs and tiered pricing down to FOB prices that compete with larger Vietnamese and Indonesian mills on mid-volume orders. Send your tech-pack, reference images, or a quick brief to our sourcing team for a same-week response with a sample plan and indicative pricing. Quanzhou Northern Garment Co., Ltd. — OEM/ODM swimwear, outerwear and activewear manufacturer based in Jinjiang, Fujian, China. Annual capacity 2,000,000+ garments. OEKO-TEX Standard 100 (year 8). Serving buyers in 20+ countries since 2013.

Designer reviewing jacket tech pack and CAD pattern drawings

Custom Jacket Manufacturing Workflow: How Production Travels from Tech Pack to Russia

08/14/2026

A custom jacket for a Russian buyer is not just a piece of outerwear. It is a cold-climate system: a heavy-duty shell, a measured amount of insulation, a tailored fit over layered garments, and a packaging plan that has to clear GOST-R paperwork at the destination port. Below is the complete workflow that takes one such jacket from the first design conversation to a fully delivered order in Moscow, and it ends where every production story should — with a buyer who has come back for a second season. 1. Design Brief and Tech Pack Development Every Russian-market jacket program starts with a written brief. For winter parkas and down jackets, that brief typically specifies a fill power target (550 to 800), a temperature rating (often minus 25 to minus 35 °C), a length preference (mid-thigh to below-knee), and the inclusion or exclusion of a real or faux fur hood trim. The tech pack that follows translates these decisions into measurable inputs: shell composition, lining weight, zipper brand and size, snap spacing, stitch length, and a full size chart in EUR and RUS gradations. Skipping this step is the single most common reason a sample round costs extra weeks. 2. Pattern Making and Grading From the approved tech pack, the pattern maker drafts a paper block in the base size, then runs it through grading software to produce the full size run — typically EU 46 through EU 60 for the Russian market, with RUS 50 through RUS 64 marked alongside. The marker is then optimized for the chosen shell width, usually 150 cm, to balance fabric yield against cut-piece handling speed. A well-built marker can save 4 to 7 percent of fabric across an 8,000-piece order. 3. Material Sourcing and Lab Testing Material sourcing — every BOM line item, from shell and insulation to zippers and snaps, is verified before it enters production. For a Russian winter jacket, the BOM typically runs to 30 to 40 line items: shell fabric, lining, insulation, hood trim, main zipper, secondary zippers, snaps, elastic tapes, drawcord, toggles, woven labels, care labels, hangtags, and polybags. Each lot is checked against OEKO-TEX Standard 100 before it enters the cutting room, and the shell goes through water-resistance, colorfastness to rubbing and perspiration, and seam-slippage tests. Insulation lots are checked for fill power and down-to-feather ratio; synthetic lots are checked for loft recovery after compression. 4. Sample Development Most Russian buyers run two to three sample rounds before signing off on bulk production. The first round, usually called a proto, verifies the silhouette and the basic construction. The second round, the fit sample, confirms grading across the size run and locks down fabric behavior. The third round, the pre-production sample, uses the actual bulk fabric and trims and serves as the contractual reference. Each round is documented with photographs and a written fit report so changes are tracked, not improvised. 5. Pre-Production Planning Once the sample is approved, the merchandising and production teams hold a pre-production meeting. The output of that meeting is a confirmed production calendar, a fabric and trim delivery plan against that calendar, and a critical-path list of the items most likely to delay shipment — usually zippers, snaps, and fur trim sourced through long-lead suppliers. Locking these early is what separates an on-time Vladivostok departure from a missed sailing. 6. Cutting Cutting — the marker is laid on layered fabric and traced before the cut is executed. Bulk fabric is laid on the cutting table in layers, typically 60 to 120 layers depending on fabric thickness. The marker is placed on top and traced, and the cut is executed either by a straight-knife machine for standard shells or by a computer-controlled cutting machine for high-precision panels such as yokes, sleeve tops, and hood pieces. Each bundle — one bundle per size and per cut panel — is barcoded and routed to the correct sewing line. 7. Embroidery and Print Application Embroidery — brand logos and back graphics are digitized, hooped, and stitched before the panels go to sewing. If the buyer's logo or back graphic is part of the design, embroidery files are digitized to match the chosen thread color and fabric weight. Logo placement is usually the left chest, the right sleeve, or the back yoke. Print applications — typically TPU film or screen print — are heat-pressed after sewing, not before, so the print covers the seam and the final shape rather than the flat panel. 8. Sewing Assembly Sewing line — a winter jacket runs through 25 to 35 sequential operations, each with its own QC check. A single winter jacket can run through 25 to 35 sequential operations on the sewing line. The order matters: shell panels are joined first, insulation is set and stitched into chambers, the lining is attached, the zipper is inserted, and the hood, pockets, cuffs, and hem are closed in the final stages. Each operation has its own QC check — seam alignment, stitch density, no missed stitches, no fabric distortion — and most lines run a QC auditor at the end of every 30 to 50 pieces. 9. Insulation Filling For down jackets, filling is done by weight per size, with grams calibrated to the fill-power target and the design temperature rating. Filling machines weigh each jacket as the down is blown into chambers, and the operator verifies that the chambers are evenly distributed. Synthetic insulation is cut into panels of the correct gram weight and stitched into the lining. 10. Finishing Finishing covers buttonhole cutting, snap attachment, steam pressing, thread trimming, and loose-end removal. Pressing is the operation that gives a jacket its final shape, especially on the lapels, hem, and sleeve crown. A poorly pressed jacket reads as cheap regardless of how well it was sewn. 11. Final Quality Inspection Inspection happens twice. A 100 percent inspection is run on every jacket for visual and functional defects — broken stitches, fabric flaws, misaligned pockets, loose snaps, zipper function. A second inspection is run as an AQL audit on a statistical sample drawn from the packed shipment, with measurements checked against the original tech pack tolerances. Anything that fails either round is either repaired on the spot or marked for rework and re-inspected before packing. 12. Packing and Labeling Approved jackets are folded to spec, polybagged with silica desiccant, and packed into individual boxes or master cartons depending on the buyer's retail channel. Russian-market cartons require care labels in Russian (or bilingual), country-of-origin labeling that meets EAC rules, and a barcode format compatible with the buyer's warehouse system. Master cartons are weighed and labeled with the same data plus the gross weight for the freight forwarder. 13. Shipping to Russia Shipping — export cartons palletized, labeled, and routed through sea freight to Vladivostok or rail through the China-Europe corridor. For a full 40-foot HQ container of around 8,000 to 12,000 mid-weight jackets, the standard route is sea freight from Shanghai or Ningbo to Vladivostok (about 7 to 10 days port-to-port) followed by rail or truck transit into central Russia. Total transit time is typically 25 to 35 days from factory gate to Moscow warehouse, with 35 to 45 days for Saint Petersburg. Documentation is the slow point: commercial invoice, packing list, certificate of origin, and the EAC conformity paperwork that Russian customs require before release. Documentation errors is the most common cause of clearance delays. 14. Customer Reception and Repeat Order For a Russian buyer working on a winter delivery window, on-time arrival in Moscow is the first half of satisfaction. The second half is that the production matches the approved pre-production sample within the agreed tolerance, that the size run holds, and that the cartons open with the right mix. When both halves are met, the same buyer returns for the next season's program with the same tech pack and a small set of refinements — exactly what happened on the program this article is based on. A repeat order from a Russian winter buyer, after a clean first delivery, is the most reliable signal that a factory has earned a place in their supply chain. Closing Notes on the Russian Winter Jacket Program A full production cycle from design brief to Moscow delivery typically runs 75 to 110 days, with about 60 to 75 of those days inside the factory and the remaining 15 to 35 in transit and customs. The bottlenecks are almost always upstream: a late fur-trim shipment, a delayed zipper draw, or a fabric mill that misses a window. Factories that win repeat Russian business are the ones that lock those upstream lines early, run a disciplined sample-and-approval cycle, and treat documentation for EAC clearance as part of the production timeline rather than an afterthought at the end.
Customs broker reviewing export documents at a busy customs office with computer screen showing tax refund forms.

Duty Drawback Programs: Refund Mechanics for Export Manufacturers in 2026

08/07/2026

JINJIANG, China — Duty drawback programs allow garment exporters in major sourcing countries to recover import duties and indirect taxes paid on inputs that are subsequently re-exported. For mid-market OEM and ODM factories, properly claiming drawback can recover 2-5 percent of FOB value on typical programs, with documentation discipline as the main barrier to capture. For garment exporters in China, Vietnam, Bangladesh, India, and other major sourcing destinations, the 2026 question is not whether to claim drawback but how to maximize recovery while maintaining compliance documentation standards that meet both program requirements and buyer audit expectations. How Duty Drawback Works Duty drawback programs refund import duties and certain indirect taxes (VAT, excise) paid on imported inputs that are: Incorporated into finished goods that are subsequently exported, OR Re-exported in their original form after import For garment factories, the most common drawback claim is for imported fabrics and trims that are incorporated into garments that are then exported. The drawback refund rate depends on the destination country’s specific program rules. Country-by-Country Comparison Duty drawback programs vary significantly by sourcing destination: China: Export tax rebate (export tax rebate) refunds VAT paid on exported goods. Standard rate 13 percent for most textile categories. This is a critical margin component for Chinese garment exporters and is well-established in standard export documentation. Vietnam: Duty drawback program for imported inputs used in exported goods. Refund rates depend on specific product categories and FTAs. Documentation requirements are stringent. Bangladesh: Duty drawback program allows refund of import duties on inputs used in exported garments. Refund rates vary by product type and FTAs. Recent program updates have expanded coverage. India: Duty drawback program has multiple rate structures depending on whether the destination is an FTA partner. Documentation is complex but well-supported by freight forwarders. For mid-market garment exporters, the destination country’s drawback rate is a significant factor in overall cost competitiveness. Documentation Requirements Drawback claims require consistent documentation linking imported inputs to exported finished goods: Import documentation: Customs entry documents, commercial invoices, packing lists, and bills of lading for imported inputs. Manufacturing records: Bill of materials showing imported inputs incorporated into specific export shipments. Export documentation: Commercial invoices, packing lists, and bills of lading for exported garments. Reconciliation: Periodic reconciliation of imported inputs against exported finished goods, with inventory accounting for any unused inputs. The reconciliation process is where most factories struggle. Inconsistencies between imported input volumes and exported finished-goods volumes trigger customs audits and potential drawback denials. Common Drawback Mistakes For garment exporters, the most common drawback mistakes are: Inadequate inventory tracking: Failing to account for inputs that were imported but used in domestic-market production rather than exports. Wrong HS code classification: Misclassifying imports or exports in a way that disqualifies them from drawback. Missing FTZ or bonded warehouse procedures: For high-volume importers, using Free Trade Zones or bonded warehouses can simplify drawback but requires specific procedures. Late or incomplete filings: Most drawback programs have strict filing deadlines. Late filings result in forfeited refunds. Insufficient buyer-side documentation: Some drawback programs require buyer-side confirmation of destination, which can be difficult to obtain. Practical Recommendations For a garment exporter maximizing drawback recovery in 2026: Build a reconciliation system that tracks imported inputs to exported finished goods with high accuracy. Spreadsheet-based systems work for low-volume programs; ERP-based systems are appropriate for higher volumes. Engage a specialized freight forwarder with drawback expertise. Most general freight forwarders lack the specific knowledge needed for maximum drawback recovery. Review HS code classifications periodically. Misclassification is the single most common cause of drawback denials. Track FTAs — garments exported to FTA partner countries may qualify for additional preference programs beyond standard drawback. File on time — most drawback programs have monthly or quarterly filing windows with no exceptions for late filings. The Bottom Line Duty drawback programs can recover 2-5 percent of FOB value for typical garment export programs, with the destination country’s specific rate a significant factor in overall cost competitiveness. The main barrier to maximum drawback recovery is documentation discipline, particularly the reconciliation of imported inputs against exported finished goods. Garment exporters that build effective reconciliation systems and engage specialized freight forwarders will capture the most drawback benefit available in 2026.

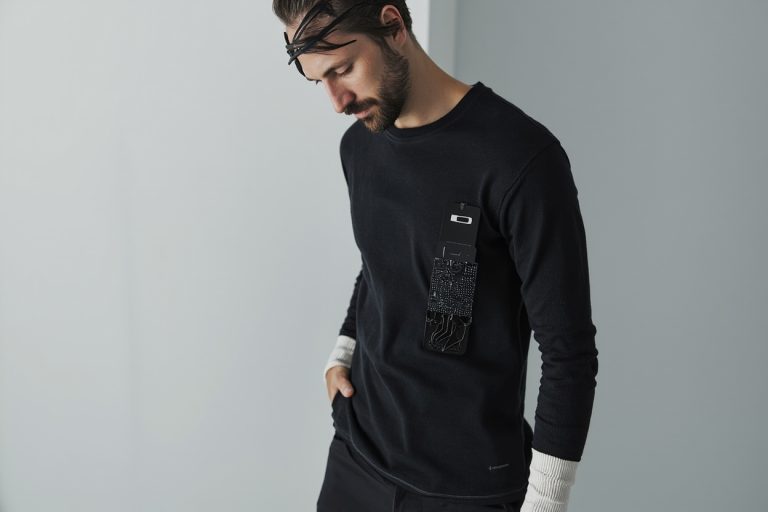
Smart garment with embedded electronic sensor strip and conductive thread, minimalist product photography.

Smart Textiles and Embedded Electronics: Market Sizing and Compliance

08/07/2026

JINJIANG, China — Smart textiles — garments with embedded sensors, conductive threads, or electronic components — have moved from research labs into commercial production over the past three years. For mid-market garment exporters, the 2026 question is no longer whether smart textiles are real, but which product categories are commercially viable and what compliance requirements apply. The smart textile market spans a wide range of applications, from fitness tracking (heart rate, motion, temperature) to medical monitoring (chronic conditions, post-surgical recovery) to industrial safety (worker location, environmental sensing). The compliance and quality requirements vary significantly across these categories. Market Sizing The global smart textile market reached approximately USD 6 billion in 2025, with the largest application categories being: Fitness and sports: USD 2.5 billion — primarily heart rate monitoring shirts, motion-tracking shorts, and temperature-regulating activewear Medical and health: USD 1.5 billion — remote patient monitoring, chronic disease management, post-surgical recovery garments Industrial and safety: USD 1 billion — worker safety monitoring, location tracking in hazardous environments Military and first responder: USD 500 million — specialized applications in defense and emergency response Other (fashion, gaming, lifestyle): USD 500 million — emerging applications with smaller unit volumes The market is growing at 15-20 percent annually, with the strongest growth in medical and health applications where remote monitoring is increasingly reimbursed by healthcare systems. Compliance Requirements by Application The compliance requirements for smart textiles vary significantly by application category: Fitness and sports: Generally subject to consumer electronics compliance (FCC in the US, CE-RED in the EU, etc.) plus general textile compliance. Medical claims should be avoided unless the product is actually registered as a medical device. Medical and health: Subject to medical device regulations (FDA in the US, MDR in the EU, NMPA in China, etc.). Class I or Class II medical device registration may be required depending on the product’s intended use. Industrial and safety: Subject to PPE regulations in the EU (PPE Regulation 2016/425) and equivalent US regulations (OSHA requirements). May require third-party certification. Military and first responder: Subject to specific government procurement requirements and certifications. Production Challenges for Garment Exporters For a garment factory considering smart textile production in 2026, the main challenges are: Sensor integration: Embedding electronic sensors into garments requires new production capabilities and quality control processes. Wash durability: Sensors and conductive threads must survive repeated washing cycles, which is technically demanding. Battery and power management: Most smart textiles require batteries, with associated shipping, safety, and end-of-life considerations. Data privacy and cybersecurity: Smart textiles that collect biometric data face data privacy regulations (GDPR, US state privacy laws, etc.) and cybersecurity requirements. Repairability and end-of-life: Smart textiles are harder to repair and recycle than conventional garments, creating sustainability concerns. Practical Opportunities for Mid-Market Factories For a factory looking to enter smart textile production, the most accessible entry points are: Partnership with established sensor companies: Rather than developing sensors in-house, partner with companies that make washable textile sensors. Several commercial options exist. Fitness and sports applications: Lower regulatory burden than medical applications, with established buyer demand from sportswear and athleisure brands. Phase 1: heated garments: Heated jackets and gloves with battery-powered heating elements are a relatively simple entry point with established consumer demand. Phase 2: biometric monitoring: Fitness-focused heart rate monitoring shirts represent the next step up, with more complex sensor integration but clear consumer demand. The Bottom Line Smart textiles are a growing USD 6 billion market with strong growth in fitness, medical, and industrial applications. For mid-market garment exporters, the entry points are increasingly accessible through partnerships with established sensor companies, but compliance requirements vary significantly by application category. Factories entering smart textile production should plan for new capabilities in sensor integration, wash durability testing, and data privacy compliance.

Synthetic fleece fabric showing microfibers shedding under running water, environmental laboratory setting.

Microfiber Pollution Regulation: California AB 1628 and EU Microfiber Rules

08/07/2026

JINJIANG, China — Microfiber pollution from synthetic textile washing is now subject to regulatory action in both California and the European Union, with material implications for garment exporters serving outdoor, activewear, and fast fashion categories where synthetic fiber content is highest. For mid-market apparel brands sourcing synthetic-rich product ranges, the 2026 regulatory landscape is no longer about voluntary commitments but about binding rules with enforcement teeth. California AB 1628: Microfiber Filtration California Assembly Bill 1628, signed in 2024, requires microfiber filtration on new washing machines sold in California starting January 1, 2027. While the bill targets washing machine manufacturers, the implication for apparel brands is that synthetic garments sold in California will increasingly be washed under filtration conditions that capture a portion of shed microfibers. For garment exporters, the direct impact of AB 1628 is modest in the short term. The bill does not impose microfiber testing or certification requirements on apparel products directly. However, brands may begin to request microfiber-shed data on synthetic products, particularly for activewear and outdoor categories where the issue has received significant consumer attention. EU Microfiber Pollution Initiatives The EU has taken a different regulatory approach, focusing on: EU Strategy for Textiles and the Circular Economy (2022): Identified microfiber pollution as a priority and called for industry action, voluntary commitments, and pre-competitive research. REACH restrictions on synthetic textile microfibers: Under review as of 2026, with a potential restriction proposal expected in 2027 or 2028. Eco-design for Sustainable Products Regulation (ESPR): Includes textile products in scope, with potential microfiber-related requirements under delegated acts. The EU approach is more comprehensive than California’s, with potential requirements extending from product design to consumer information and end-of-life management. What Brands Are Doing Major outdoor and activewear brands have been active on microfiber pollution for several years. The most common responses include: Yarn selection: Use of longer filament yarns, texturized constructions, and tighter weaves that reduce shedding during washing. Fabric construction: Brushed and raised finishes tend to shed more than flat weaves; some brands are reformulating constructions to reduce shedding. Treatment chemistry: Durable water repellent (DWR) and other finishing treatments can either increase or decrease shedding depending on formulation. Consumer information: Care labeling that recommends cold water washing and lower spin speeds to reduce shedding. Take-back and recycling: Brand-operated take-back programs that capture garments at end of life, reducing the cumulative microfiber load. Testing and Documentation For garment exporters serving brands with microfiber commitments in 2026: Shed rate testing: Some brands now request microfiber shed rate testing per methodologies like AATCC TM212 or similar. Tests typically involve washing samples under standardized conditions and counting shed fibers. Construction documentation: Yarn specification, fabric construction, and finishing chemistry documentation are increasingly requested. Care labeling alignment: Care labels should be consistent with the brand’s microfiber-reduction recommendations, particularly for cold wash and gentle cycle guidance. Practical Implications for Garment Exporters For a factory serving outdoor, activewear, or fast fashion brands with microfiber commitments in 2026: Document yarn and construction choices — brands increasingly want to understand the construction choices that affect microfiber shedding. Maintain care label accuracy — cold wash and gentle cycle recommendations should be standard for synthetic-rich products. Track microfiber-related regulatory developments — EU REACH restriction proposals and ESPR delegated acts will shape compliance requirements through 2027 and 2028. Engage with buyer microfiber requests — most major brands now have microfiber-related questionnaires or technical requirements. The Bottom Line Microfiber pollution is now subject to binding regulation in California and pending EU restrictions, with material implications for apparel brands sourcing synthetic-rich product ranges. For garment exporters, the 2026 priority is documenting construction choices, maintaining care label accuracy, and tracking regulatory developments as EU REACH and ESPR evolve through 2027 and 2028.

Stacked shipping paperwork with a digital tablet displaying customs forms, freight forwarding office setting.

DDP Shipping Terms and Apparel Margins: Incoterms 2024 in Practice

08/07/2026

JINJIANG, China — The 2024 update to the International Chamber of Commerce’s Incoterms rules tightened the obligations and risk-allocation logic for DDP (Delivered Duty Paid) shipping terms. For mid-market apparel exporters, the practical 2026 question is when DDP makes sense for EU and US-bound product, and when other terms (DAP, FOB, EXW) deliver better landed-cost economics. DDP places the full responsibility for import clearance, duty payment, and final delivery on the seller. For garment exporters, this can simplify buyer relationships and reduce buyer-side administrative burden, but it also concentrates significant cost and compliance risk on the exporter. What Incoterms 2024 Changed for DDP The 2024 Incoterms update introduced several changes that affect DDP specifically: Insurance requirements: DDP now explicitly references ICC A or similar terms for cargo insurance, eliminating the previous ambiguity about insurance responsibility under DDP. Security clearance obligations: DDP now explicitly includes security-related clearance obligations in the seller’s responsibility, particularly relevant for products subject to security screening at import. Documentation responsibilities: DDP now clarifies that the seller is responsible for both pre-shipment and post-shipment documentation, including any certificates or permits required for import. Cost allocation: DDP’s cost allocation rules are unchanged in the 2024 update, but the updated insurance and security clarifications affect the practical total cost burden on the seller. When DDP Makes Sense for Garment Exporters DDP is generally most useful in the following situations: Small-volume buyers with limited import infrastructure. A buyer without customs brokers or import compliance resources benefits from the seller handling the full import process. Buyers new to international sourcing. Brands entering the import business for the first time benefit from DDP during the learning phase. Specific regulatory environments with high import compliance complexity. Some destinations (Brazil, India) have complex import regimes where the seller’s local expertise on DDP can be valuable. Pre-cleared and pre-paid programs. Some brands use DDP for specific programs where the landed cost is fixed in advance, with the seller absorbing any duty or clearance variation. When DDP Doesn’t Make Sense DDP is generally less suitable in these situations: Large-volume buyers with established import infrastructure. Major brands typically prefer DAP or FOB, retaining control over their own import clearance and duty payment. Buyers with specific customs broker relationships. Buyers who use preferred brokers benefit from those relationships under non-DDP terms. Products subject to destination-specific quotas or restrictions. Buyers with quota allocation need to retain control of their own imports. Variable duty environments. Destinations with frequent duty rate changes (e.g., ongoing Section 301 adjustments) make DDP risky for the seller. Margin Implications For a garment exporter offering DDP terms, the margin implications are: Direct cost pass-through: Most major brands expect DDP pricing to include all duties and clearance costs as a pass-through, with no margin on those components. Risk buffer: Sellers typically include a 3-7 percent risk buffer in DDP pricing to cover duty rate changes, clearance delays, and unexpected charges. Cash flow impact: DDP terms push payment of duties and clearance costs to the seller, with reimbursement typically 30-60 days after shipment. This affects seller cash flow. Compliance liability: Under DDP, the seller is liable for import compliance failures, including any penalties or seizure events. Practical Recommendations For a garment exporter negotiating 2026 terms with mid-market buyers: Default to DAP or FOB for established large-volume buyers, unless the buyer specifically requests DDP. Offer DDP selectively for small-volume buyers, new-to-import buyers, or specific regulatory environments where the seller has expertise. Include risk buffers in DDP pricing — typically 3-7 percent on top of the expected duty and clearance cost. Maintain duty rate monitoring for key destinations, particularly the US (Section 301 changes), EU (CBAM, anti-dumping), and any destination with frequent policy changes. Document the cost components in DDP pricing so buyers can see the breakdown and understand what they are paying for. The Bottom Line DDP shipping terms simplify buyer relationships and reduce buyer-side administrative burden, but concentrate cost and compliance risk on the seller. The 2024 Incoterms update clarified insurance and security obligations under DDP but did not change the fundamental cost-allocation logic. For mid-market garment exporters, DDP makes sense for small-volume buyers and specific regulatory environments, while established large-volume buyers typically benefit from DAP or FOB terms.

Garment factory production line with workers sewing children's outerwear, organized workstations.

Bangladesh RMG Wage Developments: 2024-2026 Cost Trajectory

08/07/2026

JINJIANG, China — Bangladesh’s ready-made garment (RMG) sector remains the lowest-cost major sourcing destination for mid-market apparel, but the cost trajectory has shifted materially over the past three years. Annual wage revisions, compliance investments, and currency movements have all contributed to a 25-30 percent cumulative increase in Bangladesh RMG labor costs since 2022. For mid-market apparel brands running multi-country sourcing strategies, the practical 2026 question is not whether Bangladesh remains cost-competitive, but how the cost gap with Vietnam and China has narrowed and which product categories are still most cost-effectively produced in Bangladesh. Wage Trajectory 2022-2026 Bangladesh RMG wages are set through a tripartite process involving the government, factory owners’ associations, and worker representatives. The minimum wage was revised in late 2023, with the new wage structure taking effect in stages through 2024: Pre-2023 minimum wage: Tk 12,500 per month (approximately USD 113 at 2023 exchange rates) Post-2023 minimum wage: Tk 12,500 (Tier 1) to Tk 38,000 (Tier 7) per month, depending on skill grade (approximately USD 113 to USD 345 at 2024 exchange rates) Annual increment structure: 5 percent annual increment on the base wage, plus inflation adjustments in some years The 2023 revision represented a substantial increase at the upper skill tiers, with Tier 7 wages rising by approximately 50 percent. The lower-tier increases were more modest, in the 25-30 percent range. Compliance Cost Increases Beyond wage increases, Bangladesh RMG factories have seen substantial increases in compliance costs since 2022: Accord and Alliance inspections: Building safety remediation costs continue for many factories, with remediation budgets typically running $1-3 million per affected factory. Worker welfare and benefits: Increased contributions to worker provident funds, gratuity schemes, and health insurance have added 1-2 percent to total labor cost. Energy and utility costs: Bangladesh power tariffs have increased by approximately 20 percent since 2022, with corresponding impact on factory utility costs. Insurance premium increases: Fire and building insurance premiums have increased materially for factories in high-rise buildings, reflecting industry-wide risk reassessment. Currency Effects The Bangladeshi taka has been relatively stable against the US dollar over the past three years, with modest depreciation of 2-4 percent annually. This stability has allowed factories to absorb wage and compliance increases without major margin compression. The Indian rupee, by contrast, has been more volatile, and the Vietnamese dong has been actively managed by the State Bank to maintain export competitiveness. The Bangladesh approach of letting the taka depreciate modestly has been a factor in maintaining cost competitiveness. Cost Comparison with Vietnam and China For a representative mid-market woven shirt in 2026: Bangladesh direct labor: USD 0.65-0.85 per shirt Vietnam direct labor: USD 0.85-1.10 per shirt China direct labor: USD 1.10-1.40 per shirt The Bangladesh cost advantage in direct labor has narrowed from approximately 50 percent over Vietnam in 2020 to approximately 25-30 percent in 2026. The narrowing reflects wage increases in Bangladesh, wage stability in Vietnam and China, and the relative impact of compliance costs on each country. What This Means for Sourcing Strategy For mid-market brands running sourcing strategies across Bangladesh, Vietnam, and China in 2026: Bangladesh remains the cost leader for basic woven and knit apparel. The cost gap with Vietnam and China persists, particularly for cotton-rich basic programs. Bangladesh is less competitive for complicated outerwear and short-lead-time production. Lead times of 6-10 weeks and limited technical outerwear capacity favor Vietnam and China. Bangladesh is less competitive for technical compliance certifications. Factories with current GOTS, OEKO-TEX, and ISO 14001 certifications are concentrated in Vietnam and China. Multi-country sourcing strategies are increasingly the norm. Most major brands now run Bangladesh for basic cotton programs, Vietnam for knitwear and US-bound product, and China for complicated outerwear. The Bottom Line Bangladesh RMG labor costs have risen by 25-30 percent since 2022, with annual wage revisions, compliance investments, and utility costs all contributing. Bangladesh remains the lowest-cost major sourcing destination for basic woven and knit apparel, but the cost gap with Vietnam and China has narrowed. Multi-country strategies that match product category to country cost structure will continue to be the most resilient approach for mid-market brands in 2026.